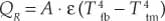Working Guide to Process Equipment, Third Edition
Next to the efficiency of the trays in a distillation tower, the efficiency of a fired heater is the most critical factor in saving and/or making money for the process plant. The primary objectives in operation of a fired heater are to
Keep the fire in the firebox
Avoid excessive heat density in the firebox
Maximize the process heat absorption for a given amount of fuel
These objectives are equally important in the operation of fired boilers whose principles of operation on the fire-side and flue-gas side are essentially the same as those of process-plant-fired heaters.
The two governing modes of heat transfer in the construction of a fired heater are radiation and convection.
In the firebox, heat transfer by radiation reigns supreme governed by Lambert s laws, as follows:
| () | |
| where Q R | = radiant heat-transfer rate, Btu/h |
| A | = surface area of the radiant tubes in the firebox, ft 2 |
| ? | = emissivity factor |
| T fb | = absolute temperature, Rankin, of the radiant surface, which is essentially the firebox temperature. The reason for this is that the flames heat not so much the tubes as the refractory, and the refractory then reradiates the heat to the tubes, so the main heat source becomes the refractory |
| T tm | = the receiving metal absolute temperature, Rankin (this is the radiant tube metal or tube skin temperature). (Rankin = F + 460) |
The amount of heat transferred to the process fluid in the convective section of a heater is governed by